China Top CNC Milling Parts Manufacturer for Global Buyers
For global buyers, choosing a China-based Cnc Milling Parts manufacturer involves more than comparing prices. It requires evidence of process control, engineering experience, and dependable communication. A capable supplier should understand aluminum, stainless steel, brass, titanium, and engineering plastics. Each material responds differently under cutting pressure.
Mike Lynch, a recognized CNC programming educator, describes the practical priority this way: “CNC machining is about consistency, repeatability, and control.” That principle remains important when a component must fit a housing, align with a shaft, or perform inside a demanding assembly. Buyers should examine machining tolerances, surface finishes, inspection methods, and production capacity. Clear drawings help, but experienced engineers still ask questions before cutting metal.
Details matter.
A reliable Cnc Milling Parts manufacturer can provide material certificates, first-article inspection reports, dimensional records, and traceable production updates. Modern equipment helps, yet machines alone do not guarantee quality. Skilled operators, calibrated measuring tools, and disciplined workflow also influence the final result. Sample parts should reveal clean edges, accurate holes, consistent threads, and controlled burr removal.
China offers strong manufacturing resources and competitive production costs. However, every supplier is not equally prepared for international projects. Some websites promise tight tolerances without showing inspection evidence. That deserves caution. Global buyers should review technical drawings together, confirm packaging requirements, and test communication speed before placing a large order. No supplier is perfect. A thoughtful partnership leaves room for feedback, correction, and process improvement. This guide explores how to evaluate China’s Cnc Milling Parts manufacturers with practical standards, realistic expectations, and greater confidence.
Definition and Scope of CNC Milling Parts for Global Buyers
China Top CNC Milling Parts Manufacturer for Global Buyers
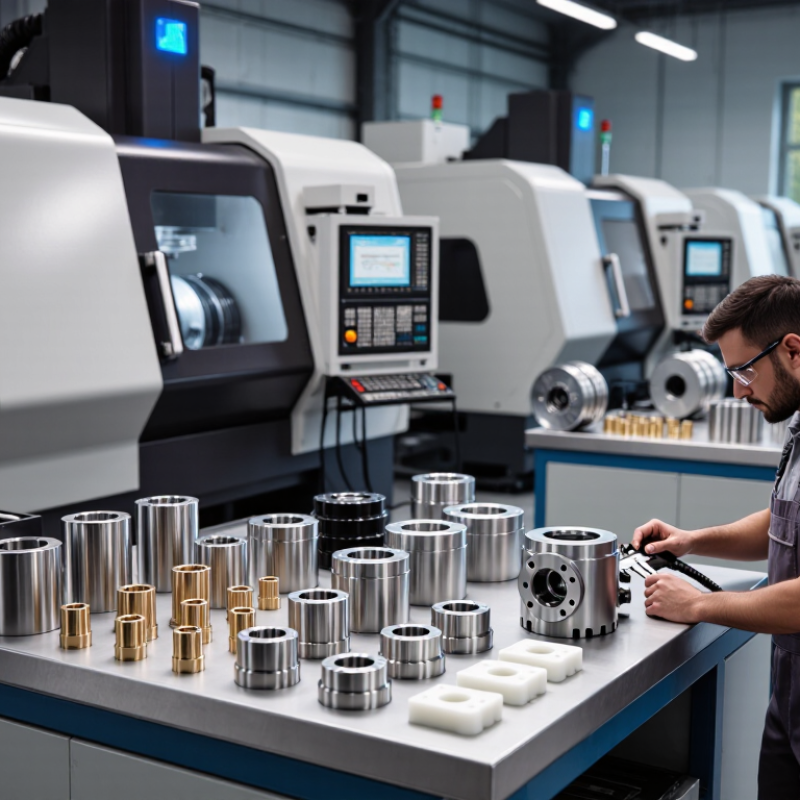
CNC milling parts are solid components shaped by rotating cutting tools under computer control. The machine removes material from metal, plastic, or engineered composites. Tool movement follows digital instructions from a technical drawing or three-dimensional model. Common operations include slotting, drilling, pocketing, contouring, and thread milling. Parts may contain flat faces, deep cavities, curved profiles, or several datum surfaces.
The scope covers prototypes, replacement components, low-volume orders, and repeated production batches. Global buyers often request aluminum housings, steel brackets, precision plates, plastic covers, and custom fixtures. Size, tolerance, surface finish, material grade, and quantity define the manufacturing route. A reliable supplier should review drawings before cutting metal. This review can identify thin walls, sharp internal corners, difficult setups, or unrealistic tolerances.
Small details matter.
Experienced production teams connect programming, machining, inspection, and packing. They may use calibrated measuring tools, coordinate measurement equipment, and documented inspection records. Material certificates and process traceability support consistent purchasing decisions. Yet a polished sample does not prove stable production. That assumption needs testing. Buyers should confirm first-article results, critical dimensions, burr control, and packaging protection. Unclear datums can create costly errors.
I have seen a single missing tolerance change the entire inspection result. Communication remains part of the technical scope, not an administrative extra.
Process Capabilities: 3-, 4-, and 5-Axis Milling at ±0.01 mm Tolerance
China Top CNC Milling Parts Manufacturer for Global Buyers
Three-, four-, and five-axis milling support different production challenges. Three-axis machining suits flat faces, pockets, and simple brackets. Four-axis machining reaches multiple sides with fewer setups. Five-axis milling can machine complex contours while reducing repositioning errors. For critical parts, our practical target is ±0.01 mm, supported by calibrated inspection equipment and controlled cutting conditions.
The tolerance is not guaranteed by machine settings alone. Material stress, tool wear, temperature, clamping force, and datum selection all matter. ISO 230-2 defines methods for evaluating machine-tool positioning accuracy, while ISO 286-1 provides the basis for tolerance systems. Deloitte’s 2024 manufacturing outlook reports that 86% of surveyed executives expect smart-factory initiatives to drive competitiveness within three years. That supports digital inspection, yet software cannot correct poor fixturing. In real production, a perfect first article is possible, but repeatability needs evidence. Sometimes, we still find small variation after apparently stable machining.
Tips: Send complete 2D drawings, 3D files, material grades, and datum requirements. Mark critical dimensions clearly. Ask for CMM results when ±0.01 mm affects assembly. Request a first-article check before batch production. Also, avoid demanding tight tolerances everywhere. It increases cost and may not improve function.
Material Selection and ISO 2768 Tolerance Standards for Milled Parts
China Top CNC Milling Parts Manufacturer for Global Buyers
Material choice controls machining stability, surface quality, and tolerance performance. The United Nations Industrial Development Organization’s 2024 statistics place manufacturing at about 16% of global GDP. This scale increases demand for repeatable milled parts.
Aluminum suits lightweight housings and offers fast cutting. Stainless steel resists corrosion but creates more heat during machining. Brass machines cleanly, while engineering plastics can deform under clamping pressure. ISO 2768-1 defines general tolerances when drawings lack individual limits. Under the medium class, a 30–120 mm linear dimension commonly allows ±0.3 mm. A 120–400 mm dimension commonly allows ±0.5 mm. These limits are useful, but not universal. Functional surfaces may need tighter controls.
I have seen drawings that looked complete yet hid one costly assumption. The machine was accurate. The material condition was not. Tool wear, thermal growth, grain direction, and post-machining stress can change results. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. Automation improves repeatability, but it cannot replace clear material and tolerance decisions.
Tips: State the material grade, hardness, and temper. Mark critical dimensions separately from ISO 2768 defaults. Ask for a first-article inspection on unfamiliar geometries. Check thin walls after deburring. Measure parts at a controlled temperature. A small review can prevent a large rework bill.
Supplier Qualification Through ISO 9001, PPAP, and CMM Inspection
A qualified CNC milling supplier must prove more than cutting speed. The ISO Survey 2022 recorded 1,265,216 ISO 9001 certificates worldwide. This scale shows quality certification is common, but certification alone is not proof of process control. Buyers should inspect the quality manual, corrective-action records, and revision history. Ask how operators handle a changed drawing.
PPAP provides that evidence in a structured format. A supplier should submit material certificates, process flow charts, control plans, capability results, and approved samples. For a machined aluminum housing, the submission should identify each critical bore, tolerance, surface finish, and inspection method. Production parts must match the approved process. Not just the sample. That detail matters.
CMM inspection adds measurable verification. A calibrated coordinate measuring machine can check true position, flatness, and complex profiles against the CAD model. The report should show datum alignment, probe qualification, temperature conditions, and actual readings. A pass or fail label is too weak. However, even strong records can hide poor sampling or operator mistakes. Buyers should review raw data and repeat selected measurements. Imperfect systems deserve questions. Supplier qualification is never a one-document decision.
Supplier Qualification Reference Points for CNC Milling Parts
This reference chart compares three objective elements commonly used in supplier qualification: ISO 9001 is structured around 7 quality management principles, PPAP defines 5 submission levels, and a standard CMM records measurements across 3 Cartesian axes—X, Y, and Z. These counts are reference points rather than supplier performance scores.
Global Purchasing Metrics: MOQ, Lead Time, Incoterms, and Quality Data
Global buyers need more than a low quotation when sourcing CNC milling parts. A reliable manufacturer should state the minimum order quantity clearly, including whether prototypes follow different rules. For example, one to ten samples may be accepted before batch production. Lead time should separate programming, machining, inspection, and packing. A typical schedule might be 7 days for samples and 20 days for repeat orders. These figures are estimates, not promises. Material availability can still change them.
Incoterms must match the buyer’s purchasing process. EXW may reduce the supplier’s responsibility, while DAP can simplify delivery planning. Confirm who pays freight, insurance, import duties, and destination handling. Quality data should be measurable. Request dimensional inspection reports, material certificates, surface-finish readings, and batch traceability. Experienced production teams also explain their measurement equipment and calibration intervals. A perfect report is less useful if the inspection method remains unclear.
Tips: Ask for a sample inspection report before ordering. Define critical dimensions with tolerances. Check packaging details, such as foam separation and moisture protection. Keep one approved sample for future comparison. I have seen schedules fail because drawing revisions were not controlled. That small mistake deserves attention. Tie payment milestones to documented production stages, not vague completion dates.
China Top CNC Milling Parts Manufacturer for Global Buyers - Global Purchasing Metrics: MOQ, Lead Time, Incoterms, and Quality Data
Indicative purchasing benchmarks for custom CNC-milled parts. Actual values depend on geometry, material, surface finish, inspection requirements, order volume, and shipping destination.
| Purchasing Dimension | Typical Benchmark | Common Range | Buyer-Side Data Requirement | Commercial or Quality Consideration |
|---|---|---|---|---|
| Minimum Order Quantity (MOQ) | 10–50 pieces for repeatable CNC milling orders | Prototype: 1–10 pieces Low volume: 10–100 pieces Production: 100+ pieces | Confirm whether MOQ applies per part number, material, finish, or total order value. | Prototype orders generally have a higher unit price because programming, setup, tooling, and inspection costs are distributed across fewer parts. |
| Prototype Lead Time | 5–10 business days after drawing and material approval | 3–15 business days | Define whether lead time starts after purchase-order receipt, drawing approval, or payment confirmation. | Complex 5-axis work, special alloys, tight tolerances, and outsourced finishes can extend the schedule. |
| Production Lead Time | 15–35 business days | 10–45 business days | Request a production schedule covering material procurement, machining, finishing, inspection, and packing. | Lead time should exclude or clearly identify international transit time and customs clearance. |
| Material Availability | Aluminum and standard steels: usually readily available | Common alloys: 2–7 business days Specialty alloys: 2–6 weeks | Require material grade, temper or condition, applicable standard, and material certificate requirements. | Material certificates such as EN 10204 3.1 may add cost and administrative lead time. |
| Dimensional Tolerance | Approximately ±0.02–±0.05 mm for selected CNC features | General machining: ±0.05–±0.20 mm Precision features: about ±0.01–±0.05 mm | Identify critical dimensions, datum structure, geometric tolerances, and measurement method on the drawing. | Tolerance capability varies by material, part size, feature location, machine condition, and thermal stability. |
| Surface Roughness | Ra 1.6–3.2 μm for standard CNC-machined surfaces | Standard milling: Ra 1.6–6.3 μm Fine finishing: Ra 0.4–1.6 μm | Specify Ra limits by surface and state whether measurement reports are required. | Tool selection, cutting parameters, tool wear, material hardness, and finishing operations affect surface results. |
| First Article Inspection (FAI) | Recommended for new parts or major drawing revisions | One complete inspection report per part number or revision | Provide drawing ballooning, characteristic numbering, measurement equipment, and sample quantity. | FAI is particularly useful for validating process capability before volume production. |
| Dimensional Inspection Coverage | 100% inspection for critical characteristics; sampling for stable routine features | 100% critical features Sampling plan for non-critical features | Define critical-to-function, safety-related, and key characteristics in the purchase specification. | Inspection frequency should reflect risk, process stability, order volume, and customer requirements. |
| Process Capability | Cpk ≥ 1.33 when formally required | Cpk ≥ 1.00 for developing processes Cpk ≥ 1.33 for capable production Cpk ≥ 1.67 for critical features | Specify the study method, sample size, control limits, and acceptance criteria before production. | Cpk targets are contractual or program-specific requirements, not universal legal standards. |
| Defect and Rejection Target | Supplier-specific target agreed during quality planning | Common commercial target: fewer than 1,000 defective parts per million for mature repeat orders | Agree on defect classification, replacement or credit policy, corrective-action timing, and reporting format. | PPM performance should be calculated from accepted inspection data and separated by defect severity. |
| Acceptance Sampling | AQL plan defined in the purchase specification | Common references: ISO 2859-1 or ANSI/ASQ Z1.4; AQL 1.0–2.5 often used for general defects | Specify inspection level, lot size, critical/major/minor defect limits, and sample quantity. | AQL is a sampling method and does not replace 100% inspection for safety-critical or specially designated features. |
| Certificate of Conformance (CoC) | Available for controlled production orders | Issued per shipment, lot, or purchase order | Request part number, revision, lot number, quantity, inspection status, and authorized signatory. | The CoC confirms conformity to agreed requirements but is not a substitute for underlying inspection records. |
| EXW Incoterm | Seller makes goods available at the stated facility | Best suited to buyers with established local logistics control | Buyer arranges pickup, export procedures where applicable, main carriage, insurance, import clearance, and delivery. | Low quoted product price can shift substantial logistics responsibility and cost to the buyer. |
| FCA Incoterm | Seller delivers goods to the buyer's nominated carrier or agreed location | Suitable for air, sea, rail, or multimodal shipments | State the named place precisely and identify responsibility for export clearance and carrier handover. | FCA is generally more flexible than FOB for containerized or multimodal freight. |
| FOB Incoterm | Seller delivers goods on board the nominated vessel at the named port | Common for sea freight involving port-to-port shipment | Specify the named port, shipment window, export documentation, and booking responsibility. | FOB is intended for sea or inland-waterway transport and is not normally used for air freight. |
| CIF Incoterm | Seller pays cost, insurance, and freight to the named destination port | Sea or inland-waterway transport only | Confirm insurance coverage, destination port charges, import clearance, duties, and inland delivery responsibility. | Risk transfers when goods are loaded on board at origin, even though freight and insurance are paid to destination. |
| DAP Incoterm | Seller delivers to the named destination; buyer handles import clearance | Useful for door delivery when the buyer manages duties and taxes | State the exact delivery address and clarify unloading, customs brokerage, duties, and tax responsibilities. | DAP can simplify transport coordination while keeping import obligations with the buyer. |
| Packaging and Export Protection | Individual protection plus moisture-resistant outer packaging when required | Foam, separators, plastic bags, cartons, pallets, or export crates based on part risk | Specify corrosion protection, scratch prevention, labeling, carton limits, pallet requirements, and packing photos. | Packaging requirements should reflect part weight, sharp edges, surface finish, transit duration, and humidity exposure. |
| Order Tracking Data | Purchase order, part revision, lot number, quantity, and shipment reference | Traceability retained for the agreed record-retention period | Request a lot-level link between material certificate, machining batch, inspection report, and shipment. | Traceability reduces investigation time when nonconformities or field issues occur. |
| Benchmark note: Ranges are general industry planning references for custom CNC milling procurement. Buyers should obtain a written quotation and confirm capability, delivery terms, inspection criteria, and applicable Incoterms for each part and shipment. | ||||
Article Source:
Have Questions? We're Here to Help!
Give us a call at (864) 989-0566 or send us a message to discuss our testing equipment with an expert.